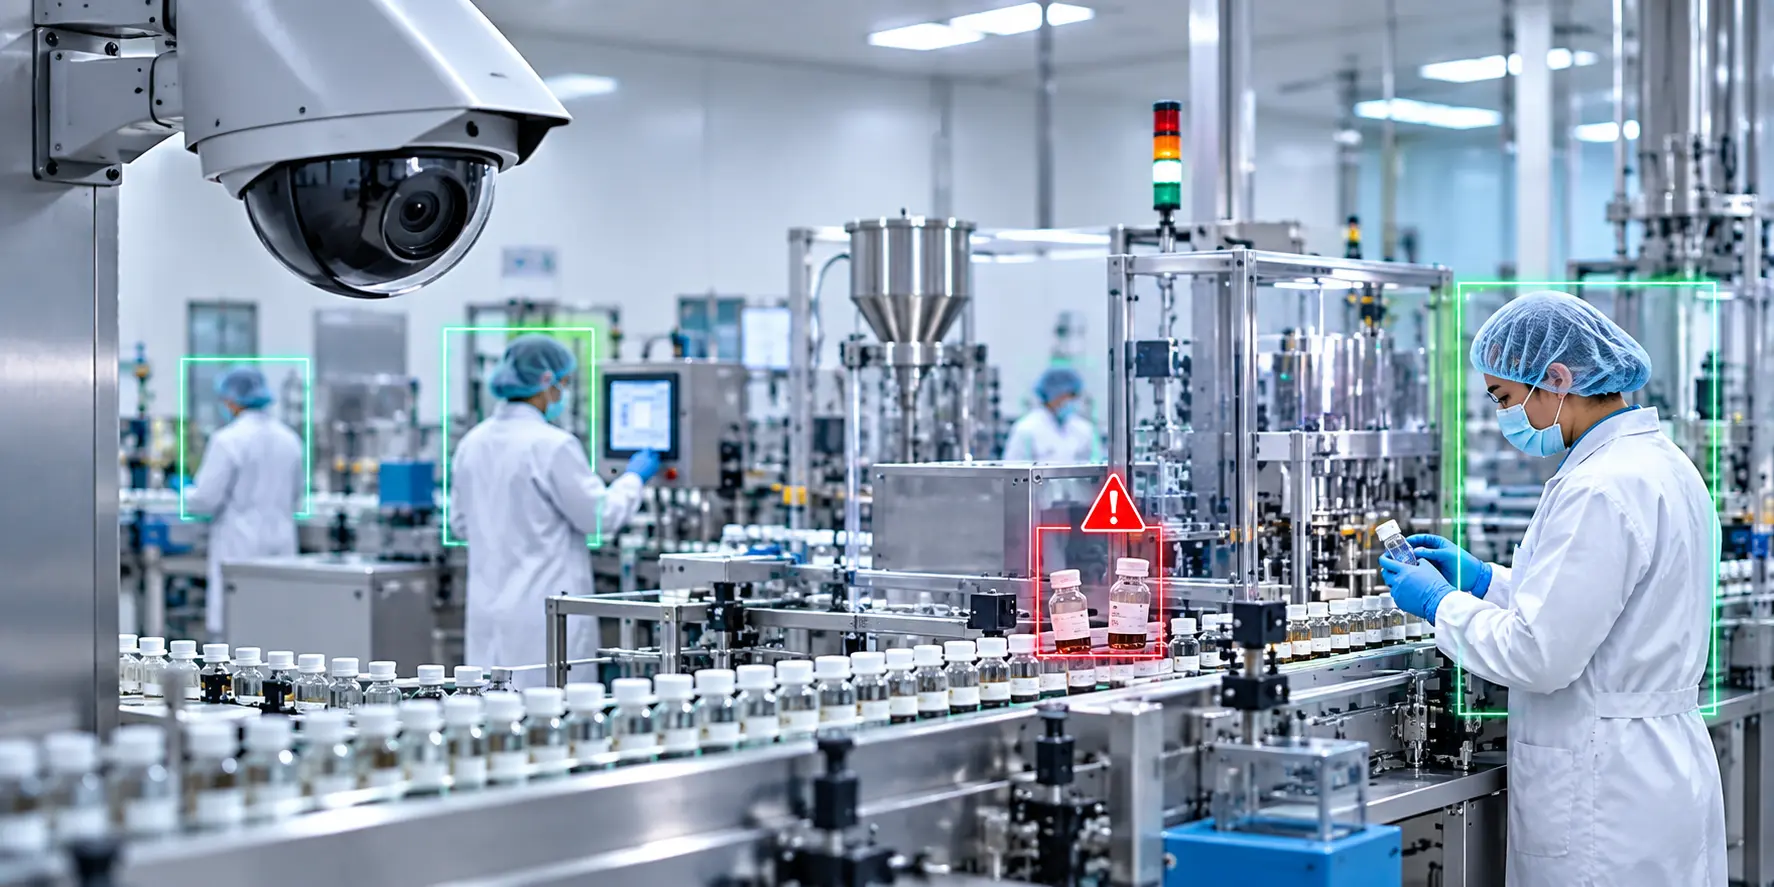
 AI Generated
Pharmaceutical manufacturing operates under some of the strictest regulatory and quality standards of any industry. A single contamination lapse, an unrecorded SOP deviation, or a security breach in a restricted zone can compromise product safety, invite regulatory action, and put patients at risk. Traditional CCTV, which only records footage for after-the-fact review, cannot keep pace with the real-time compliance demands of a modern pharma plant. This is why manufacturers are increasingly turning to AI Surveillance for Pharmaceutical Manufacturing — a proactive layer of intelligence that watches, interprets, and alerts on operational and security events as they happen.
Why Pharma Plants Need More Than Passive Recording
Pharmaceutical facilities juggle multiple risk categories at once: contamination control, GMP compliance, restricted-zone access, employee PPE adherence, and high-value raw material security. Relying on manual spot checks or reviewing hours of recorded footage after an incident is not just inefficient — it's a genuine compliance liability during audits. A modern Pharma Security System shifts this model entirely, turning every connected camera into an active observer that flags deviations the moment they occur, following the connect-configure-monitor-detect-alert workflow described in How It Works.
Rather than demanding a hardware overhaul, this approach connects directly into a facility's existing CCTV NVR and IP camera network, layering AI interpretation on top of infrastructure already in place. For a facility evaluating AI CCTV for Pharmaceutical Industry applications, this compatibility significantly lowers the barrier to deployment.
How Pharmaceutical Video Analytics Detects Risk in Real Time
At the heart of any credible AI Video Analytics for Pharma Manufacturing deployment is a continuous observe-analyze-detect-alert loop running across every camera in the cleanroom, packaging line, warehouse, and loading dock. The moment a configured rule is triggered — a missing hairnet or gloves, an unauthorized entry into a sterile zone, or unusual after-hours movement near a controlled-substance store — the system raises an immediate flag. The full breakdown of these detection and alerting capabilities is available under Key Features.
Pharmaceutical Video Analytics in this model is not generic motion detection — it is rule-based and fully customizable to the standard operating procedures unique to each facility. A cleanroom entry protocol, a gowning requirement, or a segregation rule between raw material and finished goods storage can each be configured as a distinct detection scenario, meaning the AI enforces actual SOPs rather than a one-size-fits-all template.
Monitoring Operations Beyond Security Alone
The value of AI Surveillance for Pharma extends well past theft prevention. Pharmaceutical manufacturing depends on operational consistency, and video-based intelligence gives plant managers visibility they cannot achieve by walking the floor. Automated daily reports summarize every alert and observation across shifts, giving quality and compliance teams a documented, timestamped record — useful for internal review and for demonstrating proactive monitoring during regulatory audits.
For facilities running multiple manufacturing units or warehouses, centralized visibility is essential. A multi-site management dashboard consolidates alerts, reports, and camera intelligence from every site into one interface, allowing a compliance head to oversee several plants without needing dedicated on-site monitoring staff at each location.
Detecting Risks Specific to Pharmaceutical Environments
A well-configured Pharma Manufacturing Security System is built to catch the risk categories that matter most in this industry: PPE and hygiene violations at entry points, restricted-area intrusion around API storage or R&D labs, loitering near high-value inventory, and after-hours access outside approved shift windows. Similar violation detection — including missing protective equipment flagged instantly — has already been demonstrated in real-world detection footage from an active industrial deployment, illustrating the same underlying detection logic that applies directly to pharma cleanrooms and production floors.
Because pharmaceutical plants typically run large camera networks across multiple buildings, wings, and storage areas, scale matters. An industrial-grade processing unit supporting 8+ cameras and large-scale deployments is positioned specifically for manufacturing plants, pharma facilities, and corporate campuses — making it the natural fit for enterprise-wide AI Surveillance for Pharmaceutical Plants rather than the compact device used in smaller retail or clinic settings.
Built for Compliance-Grade Reliability
Downtime is not an option in a regulated manufacturing environment, and neither is a security blind spot. A dependable Pharma Security System needs to keep functioning even when connectivity drops. On-premises video processing ensures monitoring and detection continue uninterrupted during network outages, with alerts and logs automatically synchronizing to the dashboard once connectivity is restored. For a plant operating around the clock, this internet-independent architecture means compliance monitoring never has a gap, regardless of network conditions.
Alerts are delivered instantly through WhatsApp, email, and a private dashboard, so plant supervisors and quality heads are notified within seconds — not during the next shift handover — whenever a violation or security event is detected.
The Bottom Line
Pharmaceutical manufacturing cannot afford reactive security. Every contamination risk, SOP deviation, or unauthorized access event carries downstream consequences that extend from product quality to regulatory standing. Deploying AI Surveillance for Pharmaceutical Manufacturing transforms an existing camera network from a passive recording tool into an active compliance and risk-detection system — monitoring operations, detecting risks, and ensuring security exactly as a modern pharma facility demands. Get in touch to discuss your plant's requirements and see how AI-driven video analytics can be configured around your specific SOPs.
FAQs
It continuously monitors cleanroom entry, gowning procedures, and restricted-zone access, instantly flagging deviations from configured SOPs so compliance teams can respond in real time rather than discovering violations during a scheduled audit.
It can detect PPE and hygiene violations, unauthorized access to sterile or restricted areas, loitering near high-value raw materials, and suspicious after-hours activity — all based on rules configured for the specific facility.
Yes. The system connects directly to existing CCTV NVR and IP cameras, so a pharma plant can add AI-driven detection and alerting without replacing current surveillance hardware.
Yes. Industrial-grade AI processing units supporting 8+ cameras are built specifically for large-scale deployments across manufacturing plants, pharma facilities, and multi-site campuses, with centralized dashboard monitoring for every location.
Yes. On-premises video processing keeps detection and monitoring active during connectivity loss, automatically syncing alerts and reports once the network connection is restored.
Your cameras already see everything. Patrol makes them understand everything.
Transform surveillance footage into actionable intelligence. Receive real-time alerts, ensure SOP compliance, and protect people, assets, and reputation.